 EN












The complete process at a glance
Manufacturing resin cutting discs requires coordinated material preparation, forming, curing and inspection. The press forms the mixture into blanks; curing develops the resin bond; inspection assesses whether the product meets the agreed requirements. Each stage needs appropriate verification; the appearance of the next-stage product alone is insufficient.
- 01Raw materials and weighingSpecifications, batches and feeding standards
- 02Mixing and material preparationStatus, sequence and temporary storage conditions
- 03Forming and reinforcementMold, structure and blank inspection
- 04Curing and coolingLoading, Complete Cycle and Recording
- 05Inspection and ReleaseInspection plan and result processing
- 06Packaging and warehousingIdentification, batch and order requirements
General process relationship representation. Screening, conditioning and specific sequences are adjusted according to the confirmed material system and process arrangements.
01 Raw material confirmation and weighing
First clarify the product to be manufactured, and then confirm the abrasive, resin system, reinforcing materials and supporting auxiliary materials. Even if the outer diameter is the same, the materials and processes required may be different if the product uses, thickness and structure are different.
When receiving materials, the name, specification, batch and available technical information should be checked; when weighing, clarify the mass basis used for each addition ratio. The percentage based on the abrasive mass cannot be used directly as the total mixture percentage.
Material identity
Name, grade or specification, source batch and storage requirements.
Feeding basis
Actual feed amount, proportioning basis, and adopted process version.
Batch association
Associate material batches with mixed batches to facilitate subsequent comparison testing and traceability.
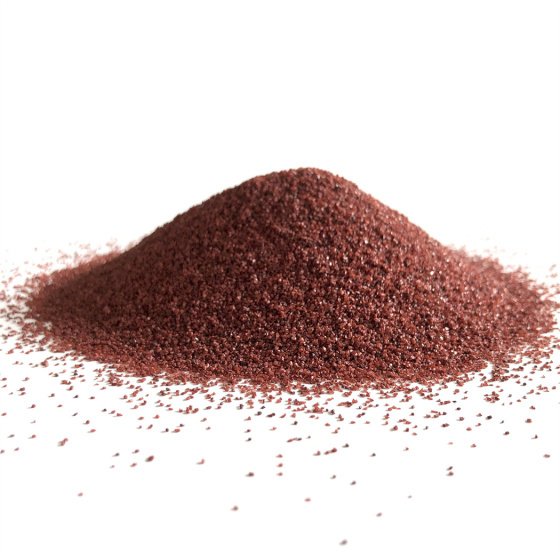
When selecting materials, you can first check Raw material catalog ↗; Specific grades and binder supply scope still need to be confirmed item by item.
02 Mixing, conditioning and transportation
The task of mixing is to combine the weighed materials in the confirmed order and conditions to obtain materials suitable for subsequent molding. When evaluating a mixer, you should look at the actual single batch feed weight, discharge method, cleaning and material changeovers, and the number of batches required per shift, rather than just comparing volume or motor power.
Whether the mixture needs conditioning and screening, as well as the corresponding sequence, should be determined according to the material system and proven technology. The temporary storage container, environment and allowed waiting time should also be connected with the molding supply to avoid having only a press plan without a mixture turnover plan.

- Record material batch, feed weight, mixing sequence and time.
- Identify mix batches, status and temporary storage conditions.
- Before changing formula or material, check cleaning, residue and transfer arrangements.
Extended reading:Mixer selection, batch uniformity and testing ↗.
03 Forming and reinforcing structure
During molding, the mixture, reinforcement mesh, bore rings and other applicable components are put into the mold according to the product structure, and then pressing and demoulding are completed. The use, number of layers and positions of components depend on the product design, and a general schematic should not be used to assume that all cutting discs have the same structure.
Assess the press and tooling together against disc diameter, thickness, bore, construction and production plan. Station count, pressing-head count, feeding and turning arrangements are distinct configuration factors. Neither machine appearance nor a single specification is enough to select the configuration.

| Inspection object | What needs to be confirmed | Why record |
|---|---|---|
| Molds and components | Model, product specifications, component structure and assembly status | Confirm that correct tooling and materials are used |
| Molding conditions | Feed benchmark, feed distribution and confirmed press settings | Provide consistent conditions for exception comparisons |
| Pressed-blank condition | Applicable inspection items such as weight, thickness, bore diameter and appearance, etc. | Process deviation found; does not replace finished product release |
Regarding the influencing factors of pressed blank thickness, you can continue reading Pressed-blank thickness control in automatic molding ↗.
04 Loading, curing and cooling
The formed pressed blank needs to be loaded in a confirmed manner and entered into the appropriate curing equipment. The curing plan should take into account the resin system, product thickness, loading method, temperature recording and cooling conditions, and cannot copy the temperature curve of another product.
When evaluating curing capacity, it depends on the number of effective loads and the complete occupancy cycle. The actual organization of furnace loading, heating, holding, unloading and cooling or transfer will all affect whether the next batch can enter in time. The furnace volume itself cannot be directly converted into the number of finished products that can be delivered per day.

Extended reading:How to Verify Curing Oven Temperature ↗.
05 Inspection, disposition and release
The inspection plan should be clear when configuring equipment: which items to inspect, what methods to use, which items to inspect piece by piece, which items to sample by batch, what requirements to judge, and how to identify and dispose of non-conforming products.
| Inspection area | Main concerns | What this does not establish |
|---|---|---|
| Appearance and size | Applicable cracks, chipping, deformation and dimensional deviations | It cannot be judged that all performances are qualified based on normal appearance alone. |
| Balance check | Measuring unbalanced conditions under specified conditions | Static balancing is not equal to dynamic balancing or full safety inspection |
| Mechanical integrity tests such as rotational strength | Evaluate the corresponding results according to the specified test conditions | Not equivalent to proven cutting efficiency or wear resistance |
| Cutting or Grinding Application Test | Evaluate actual performance under comparable working conditions | Product testing cannot be replaced by equipment rated parameters |
Test methods, sampling and acceptance criteria should be confirmed according to applicable product requirements and project agreements, and this table does not replace specific inspection procedures. When you need to organize a comparative test, you can view Trial production and test verification support ↗.
06 Packaging, batch identification and warehousing
After confirming product disposition based on the inspection results, check the specifications, quantity, label, packaging form and order requirements. Packaging should protect the product during storage and transportation, and labeling and batch information should be able to be linked to corresponding product records.
- Distinguish packaging quantity, labeling and outer box requirements according to specifications and orders.
- Clearly distinguish conforming products, products awaiting disposition and nonconforming products.
- Confirm storage, handling and transportation conditions according to material and finished product requirements.
- When batch data is required, confirm record range and file status before delivery.
How to avoid “a single machine is very fast and the entire line is backlogged” between processes?
| Observed condition | Priority Check | Required information |
|---|---|---|
| The press waits for material | Whether the mixing batch, discharging and temporary storage are connected | Actual batch size, time per batch and supply arrangement |
| The molded product is waiting for curing | Whether loading capacity, occupancy cycle and turnover tooling match | Product Mix, Effective Loading and Cycle Recording |
| Finished product awaiting release or packaging | Check whether tasks, personnel, counting and packaging rhythm are coordinated | Inspection plan, packaging specifications and work-in-progress status |
These are starting points for inspection, not identified causes of failure. When configuring a new line, the same product mix and planning period should be used to compare process capabilities, and different units or ideal peaks cannot be directly combined into daily output.
Six-stage manufacturing overview ↗ · Cutting disc production line solution ↗ · Mixing equipment ↗ · Curing equipment ↗
Choose equipment against the process requirements
Connect each stage to the proposed equipment and agreed acceptance conditions. Start with the intended cutting-disc or grinding-wheel line, then compare forming options. Product and process validation remain necessary.